Aspects of scheduling , Mechanical Engineering

Assignment Help:

Aspects Of Scheduling 

The difficulty is a modification of a flexible manufacturing cell at ABB's plant for the manufacturing of turbocharger in Baden, Switzerland. The difficulty is a little modified to make it  more demanding via eliminating one lading station (or else the average use of the loading stations is below 40 percent for full use of all machines) and via changing the part mix to acquire an extra uniform distribution of the load in the system. Two various cases are considered. In the initial condition, the original loading times and continuous order release throughout the shifts are supposed. This concludes in moderate average queue lengths. In the second condition, the loading times are raised, various load levels for machines are generated, and the orders are released merely at the starting of each shift. These results in a considerably more tough decision problem at the loading station where currently long queues exists and the that termed as shading effect occurs.

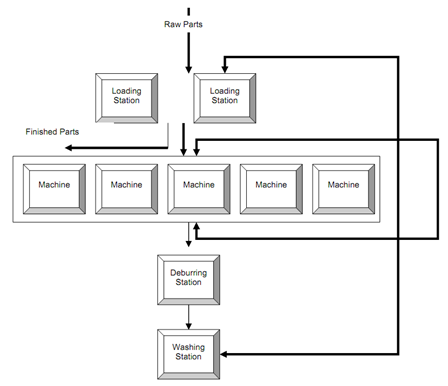
The layout of the flexible manufacturing system is depicted in following figure. Within the underlying industrial system, there are five machines and two of them identical and two loading stations, a deburring station, and a washing station. Now, this is supposed that only one loading station is obtainable, or else utilization of the loading stations is restricted to only 40 percent. All parts have to be loaded initially after that one or two machining operations obey, and after that deburring, reloading, washing, another one or two machining operations, deburring, unloading and washing.
                         1141_Aspects Of Scheduling.png

                                            Figure: Layout of FMS

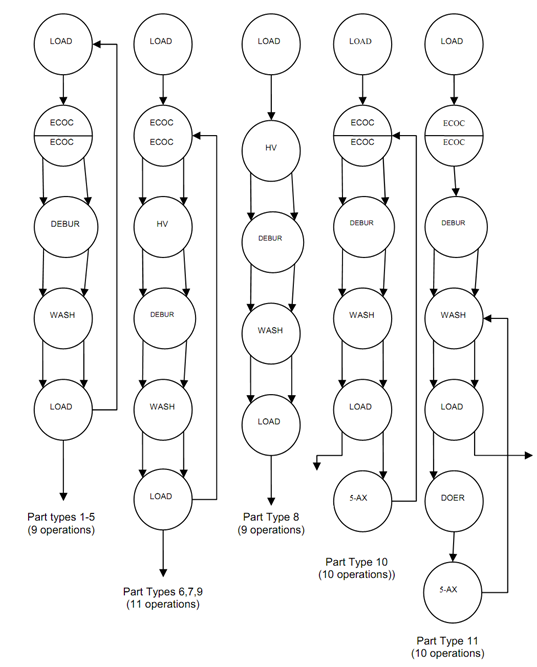
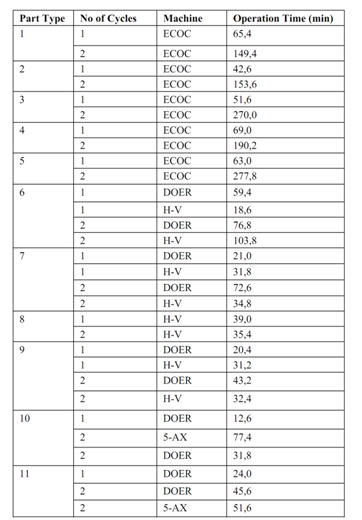
There are 11 elements types. The greatest number of operations per element type is 11, the smallest is nine. Flow diagram of all 11 elements types are represented in following figure. The operation times for machining operations are specified in Table no.1. Operation times at the stations WASH, LOAD, DEBUR are equal for all the parts. During case 1, the operation times are as:


Initial loading


8 min


Unload/reload


13 min


Final unloading


5 min


Deburring (each time)


8 min


Washing (each time)


6 min

During case 2, all the operation times on the loading stations are raised via five minutes; the other operation times keep not changed. This generates a bottleneck on the loading station through that all elements should pass three times, and thus a more demanding decision difficulty at the loading stations results.
                         1366_Aspects Of Scheduling 1.png

                                     Figure: Machining Sequences for Part Types

                                        Table no.1: Machining Times for Part Types


                                     975_Aspects Of Scheduling 2.png


Related Discussions:- Aspects of scheduling

Deficient frame and redundant frame - truss, Deficient Frame and Redundant ...

Deficient Frame and Redundant Frame - truss: Deficien t Frame: If the numbers of member in the frame are less than (2 j -3), then the frame is called as deficient fr

Loosening a part with multiple fasteners services tips, Loosening a Part wi...

Loosening a Part with Multiple Fasteners: Loosening a part with multiple fasteners should be done from the outside to inside in a criss-cross pattern, loosening the small fastener

If engine does not start in wet or damp weather, If Engine Does Not Start i...

If Engine Does Not Start in Wet or Damp Weather Causes of Problem Remedy   Insulators are not clean and dry Fuel t

Engine management system, A preamble to engine management systems for IC en...

A preamble to engine management systems for IC engines objectives, functionalities and main features

Application of hot service insulation, Q. Application of hot service insula...

Q. Application of hot service insulation? Provision for the expansion of hot equipment shall include the installation of expansion springs in circumferential banding securing i

Find out the power - hollow shaft, Find out the power - hollow shaft: ...

Find out the power - hollow shaft: A hollow shaft of internal diameter 400 mm & external diameter 450 mm is needed to transmit power at 120 rpm. Find out the power it may tran

Metals and melting practices -slag, Metals and Melting Practices -Slag,Tapp...

Metals and Melting Practices -Slag,Tapping,Vacuum Degassing Slag : A waste product of iron and steel making, utilized to eliminate impurities. In particular, a by-product o

Illustrate the importance of aesthetic consideration, You as design Enginee...

You as design Engineer, Describe how you would decide a suitable factor of safety for the design of a new mechanical elements. Illustrate the importance of aesthetic considerati

Combustion chamber and radiant section, Q. Combustion Chamber and Radiant S...

Q. Combustion Chamber and Radiant Section? The combustion chamber and the radiant heat transfer section of the Steam Generators shall be a horizontal, multiple pass arrangement

Friction, Friction: you have learnt laws of friction and problems invo...

Friction: you have learnt laws of friction and problems involving dry friction. The relative sliding motion of one body on another body is resisted by forces called as frictio

Write Your Message!

Captcha
Free Assignment Quote

Assured A++ Grade

Get guaranteed satisfaction & time on delivery in every assignment order you paid with us! We ensure premium quality solution document along with free turntin report!

All rights reserved! Copyrights ©2019-2020 ExpertsMind IT Educational Pvt Ltd